Industrial dehydration
Industrial dehydration for fruits, vegetables, specialty crops, and novel inputs, processed to your exact specifications.
From raw agricultural intake to finished, packed ingredients, our Norwood facility runs washing, industrial tunnel drying, custom processing, and packaging under one roof. Every shipment is backed by complete QA documentation, including custom specification sheets and batch Certificates of Analysis (COA).
What We Dehydrate & Process
Transforming raw agricultural products, novel proteins, and specialty crops into high-value ingredients.
Our industrial tunnel dehydration and processing lines convert fresh, frozen, or surplus agricultural inputs into shelf-stable formats designed for seamless storage, transport, and formulation.
Vegetables & Produce
Whole pieces, dices, flakes, or powders dried to your target moisture and water activity specifications.
Fruits
Dehydrated fruit pieces, granules, and powders optimized for cereals, snack bars, bakery, and beverage formulations.
Herbs & Botanicals
Leaf and stem gently dried under controlled conditions to preserve natural colour, aroma, and essential oils.
Specialty & Novel Ingredients
Novel proteins, custom blends, and functional ingredients processed and ground to exact mesh and particle size requirements.
How the line runs
Six steps from raw intake to a shipped ingredient.
Every step happens in the same building, which is what keeps lead times and handling short.
- 01
Intake
Raw product arrives, is checked, and is logged.
- 02
Wash and prep
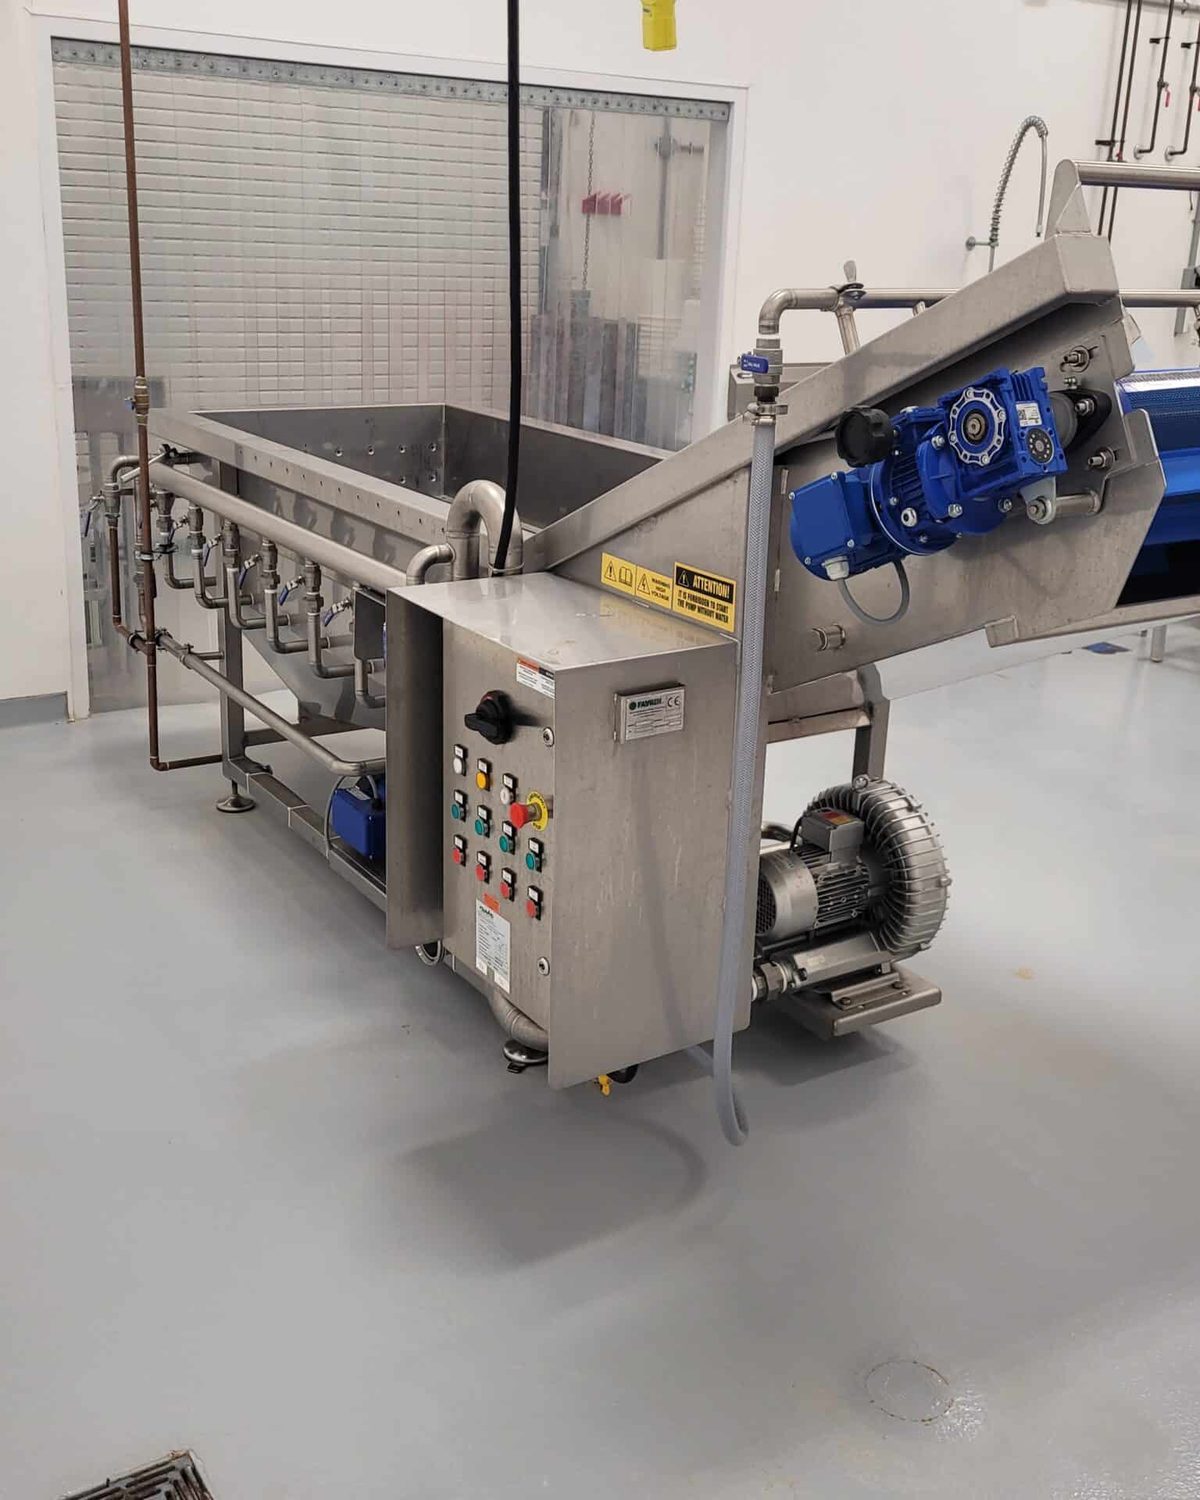
Washing and conveying lines prepare it for the dryer.
- 03
Dehydrate
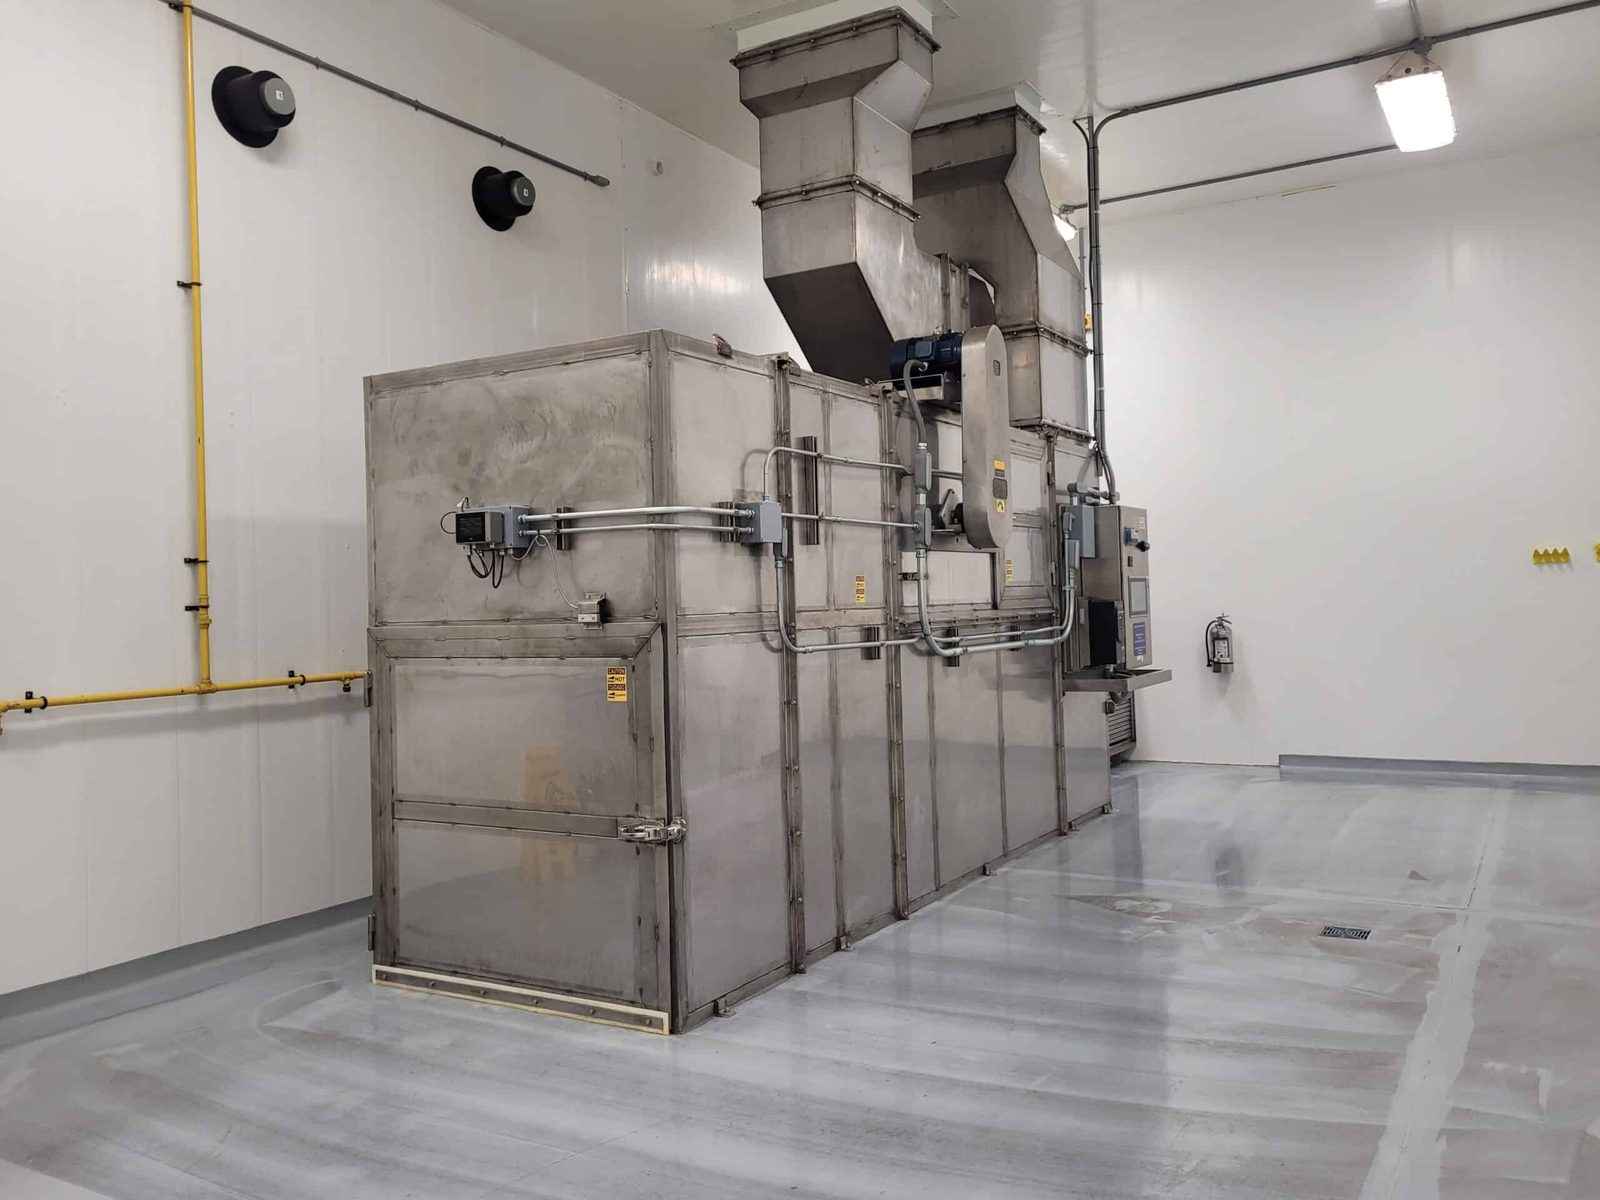
The tunnel dehydrator dries it to a shelf-stable moisture level.
- 04
Mill
Grinding to the particle size the specification calls for.
- 05
Pack
Packed on site in the formats the order needs.
- 06
Ship
Out the door to customers at home and abroad.
Equipment and premises
Built for drying at industrial volume.
The equipment list and the food-safety programme, in one place.
- Dehydration
- Tunnel dehydrator for fruits, vegetables, specialty crops, and novel inputs.
- Preparation
- Automated washing equipment and conveying lines feed the dryer.
- Milling
- Grinder for powders and flakes; particle size to specification.
- Co-packing
- Filled and sealed on site, from custom B2B bulk containers to retail-ready packaging.
- Food safety
- Safe Food for Canadians licence (CFIA)HACCP policies and procedures
- Documentation
- Specification sheet and certificate of analysis with shipments; routine microbiological testing on every batch of food product we manufacture.
- Premises
- One food-grade building in Norwood, Ontario, producing since 2014.
Co-packing
Turnkey Contract Processing & Co-Packing
Drying is just one step. We can run the entire line. Brands that need washing, freezing, dehydration, custom processing, blending, and retail-ready co-packing can hand the entire job to one team in one CFIA-licensed building. Whether you need a single processing step absorbed or a complete turnkey manufacturing solution, our Norwood plant scales with your business.
Food & Beverage Brands
On-demand processing, drying, blending, and co-packing capacity without the capital expense of building or expanding your own plant.
Consumer Packaged Goods (CPG)
Custom ingredient manufacturing and retail-ready packaging.
Pet Food & Animal Nutrition
High-purity novel proteins, dehydrated fruits, and vegetable ingredients backed by batch COAs and full safety documentation for treat and feed formulators.
Agricultural Producers & Export Markets
Value-added processing that converts raw surplus crops into shelf-stable ingredients with international export documentation.
Who uses it
Food manufacturers, ingredient companies, and pet food producers.
Dehydration capacity without building a drying room of your own.
Food & beverage
Drying, processing, and co-packing capacity without adding a plant.
Learn moreConsumer packaged goods
Manufactured ingredients for cereals, bars, snacks, and baked goods.
Learn morePet food & animal feed
Cricket protein and dried ingredients with documentation for every shipment.
Learn moreExport markets
Shelf-stable formats and the documents an international shipment needs.
Learn moreNext step
Describe what you need dried.
The product, the volume, and the timeline. A person replies within five business days with the questions that matter and the path to a quote.